

The vertical shaft impact crusher, also known as a sand making machine, handles soft, medium-hard and very hard materials — ores, cement, refractories, calcined bauxite, glass raw material, manufactured sand, stone and metallurgical slag. Its wear parts are concentrated in the rotor and crushing chamber: main throwing heads, secondary blades, upper and lower flow plates, and guard plates. Their wear rates differ sharply, so buying one alloy for the whole set usually means the cheapest part fails first while the most expensive one is barely worn. After 40 years in mining equipment and wear casting since the 1980s, the Grand Heavy team breaks down wear by component and gives a per-part material plan.

Grand Heavy wear castings — sand making machine parts share the same 40-year foundry line as crusher liners
| Quick View | Verdict |
|---|---|
| Wear part list | Main throwing heads, secondary blades, upper and lower flow plates, guard plates |
| Fastest wearing | Main throwing heads — direct impact and abrasion from high-speed material |
| Most overlooked | Flow plates and guard plates — wear changes material path and lowers product quality |
| Core logic | Select material per component by its stress type, not one alloy for the machine |
| Common models | HX, VSI and HVI series |
The core is a high-speed rotor: material falls through the central feed tube, is accelerated by the throwing heads, exits along the flow plates and strikes the material bed or anvils in the chamber at very high speed. Two operating modes are common:
Because each component sees a different stress type, per-part material selection is essential:
Grand Heavy supplies three material families: manganese steel, high chrome, and manganese plus alloy (titanium carbide inserts). Manganese work hardens under sustained impact from about HB200 to roughly HB500 at the surface; high chrome reaches as-cast carbide hardness above HRC58; the insert solution combines a titanium carbide rod zone (microhardness about 1400-2900 HV, per the certificate accompanying each batch) for wear resistance with a manganese base for impact. Manganese parts are water toughened per GB/T 5680 at about 1050 deg C [To be added: standard version year].
A manufactured sand plant reported that output had not changed but particle shape and gradation were deteriorating, with customers complaining about fluctuating fineness modulus. The machine itself ran normally, with vibration and current within range.
Inspection of the rotor revealed two problems. First, throwing head wear was badly uneven — two heads were near their limit while others were barely worn, showing that the set had not been weight paired before installation, causing rotor imbalance and inconsistent trajectories. Second, the flow plates had worn into stepped grooves, disturbing material flow so the exit angle deviated from design.
Together these meant material no longer struck the bed at the design angle, degrading both crushing and shaping — hence poor particle shape and unstable fineness modulus. The fix was to replace heads and flow plates as a complete set rather than only the two worn heads, then weight pair them and re-verify rotor balance. Product shape stabilized afterwards. Two rules came out of this: throwing heads must be replaced as a weight-matched set, and flow plates showing obvious steps must be replaced rather than run on.
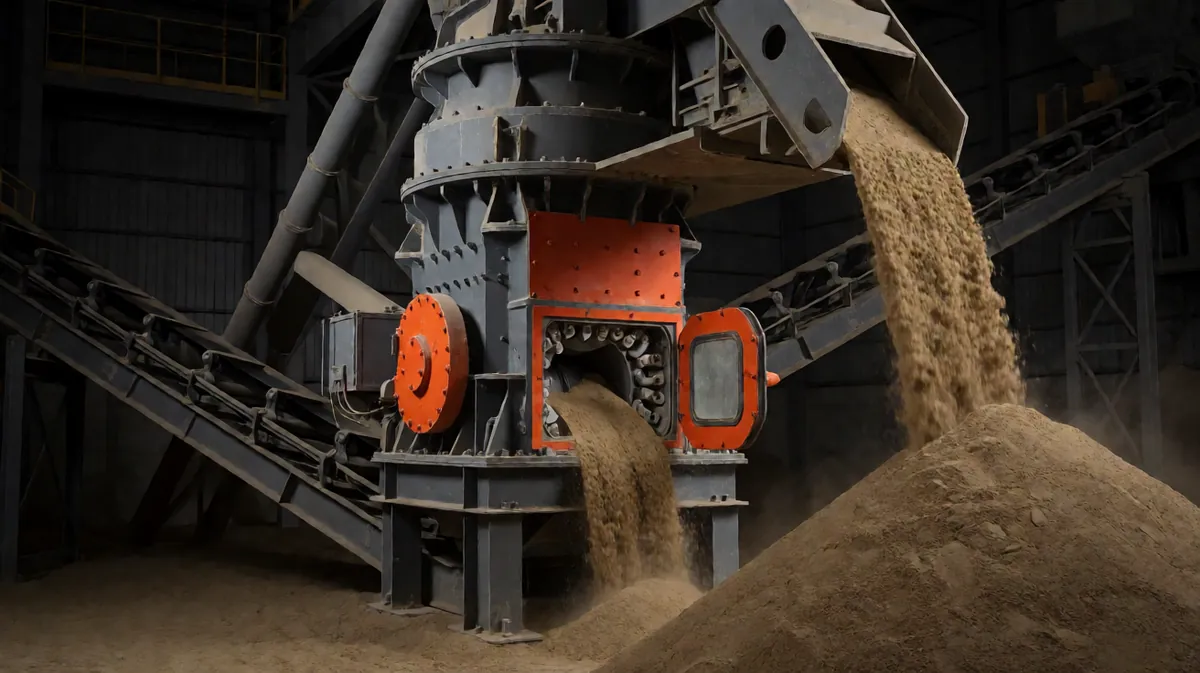
Grand Heavy wear castings — a material certificate per batch, with material selected per component
| Component | Dominant Stress | Recommended | Rationale |
|---|---|---|---|
| Main throwing head | Severe impact and abrasion | Manganese with inserts / high chrome | Must resist wear and resist cracking; highest ejection risk |
| Secondary blade | Moderate impact and abrasion | High chrome / manganese | Lower load than main heads, budget-dependent |
| Upper and lower flow plates | Sliding abrasion | High chrome (hardness first) | Low impact, high abrasion — hardness pays most |
| Guard plate | Abrasion with light impact | High chrome / manganese | Match to guide-face wear rate |
| Anvils in rock-on-iron mode | Direct impact | High chrome / manganese | Rock-on-iron wears noticeably faster than rock-on-rock |
| Hard abrasive rock, maximum life | Severe impact and abrasion | Titanium carbide inserts | Rods resist wear, base absorbs impact; 2-3x life versus standard (verify in field) |
How to use: identify each component stress type first, then match the material. Note that throwing heads and flow plates must be evaluated as a set — mismatched wear between them disturbs flow and degrades product quality even if individual parts are excellent. Actual life per component should follow your own field logs. [To be added: sand making machine wear part life logs]
| Buyer Type | Action |
|---|---|
| Budget limited | Protect alloy grade on heads and flow plates; control unit price on guard plates |
| Life focused | Titanium carbide insert heads, whole rotor replaced as a weight-matched set |
| Corporate bulk | Lock specification and weight tolerance by model, annual pricing with certificates |
The right approach is not picking the hardest alloy but selecting material per component by stress type: throwing heads need both toughness and hardness, flow plates favor hardness, guard plates follow guide-face wear. Add weight-matched set replacement and rotor balancing, and product shape and machine stability hold together. Foshan Grand Heavy Trading Co., Ltd. has built mining equipment and wear casting expertise for 40+ years, holds 20+ patents, partners with Central South University and Guangdong University of Technology, and is certified as a National High-Tech Enterprise [To be added: certificate number]. We serve CNBM, Conch Cement and clients across 6 overseas markets with 24-hour response from Guangzhou, Foshan and Changsha.
📞 Sand Making Machine Parts Selection & Custom Casting — Grand Heavy
40 Years of Wear Casting | 20+ Patents | Central South University Partnership | National High-Tech Enterprise
Trusted by CNBM & Conch Cement | 24-Hour Response from Guangzhou, Foshan, Changsha
Hotline: +86-0757-18144901190 | Email: zhouwenbin@fsgrandheavy.com
Website: www.fsgrandheavy.com
Grand Heavy — Per-part alloy selection and set replacement, protecting both shape and stability!

Crusher Wear Parts Life Reference Table: Jaw Plates, Blow Bars, Hammers, Mantles and More

5 Common Cone Crusher Failures and How to Fix Them

Advantages of the Small Hydraulic Double-Roll Sand Making Machine

Jaw Plate Buying Guide: Material Identification, Price Traps and Replacement Cycles

Beyond Material Wear: What Other Factors Shorten the Service Life of Fixed Jaw Plates?

Jaw Crusher vs Impact Crusher: Which One to Choose? A 6-Factor Comparison


Room 3411, Building 1, Xinrui Plaza, No. 10 Lianing Avenue South, Dongping Community, Lecong Town, Shunde District, Foshan City (for office use only)
18144901190 (Miss Zhou )
zhouwenbin@fsgrandheavy.com

I. The information displayed on this website is provided by the website owner, who is responsible for the authenticity, accuracy, and legality of the content.
II. If the certificates displayed on this website are expired or invalid, visitors are welcome to notify us to replace them with valid certificates. (Contact information available on this website)
III. If the information displayed on this website infringes your copyright or other legal rights, or displays any content violating national laws, please contact us (Company: Foshan Damei Smart Manufacturing Trading Co., Ltd Phone: 18144901190 Email: zhouwenbin@fsgrandheavy.com). We will review and handle within 24 hours.
The New Advertising Law stipulates that no absolute or functional terms shall appear on any page. Our company supports the New Advertising Law. In order not to affect consumers' normal purchases, we have reviewed and modified the prominent areas of our pages. We hereby solemnly declare: All absolute and functional terms on our pages are invalid before this declaration and shall not be used as grounds for compensation.
For non-prominent areas and unchecked areas, we will gradually make improvements. However, manual review cannot guarantee 100% completeness. We do not accept or compromise on any form of compensation claims based on superlative terms or online fraud in the name of counterfeit detection. Please make way for genuine consumers, as rights protection is a two-way process. We hope new and old customers understand and support us, and contact customer service to help improve.
Pursuant to the Advertising Law and instructions from the Administration for Industry and Commerce, we specially remind you that the product titles on this website are set purely for operational and technical traffic purposes and do not constitute product efficacy claims. Please do not take them out of context. Additionally, in accordance with Article 15 of the Consumer Rights Protection Law of the People's Republic of China regarding the authenticity of product promotion, as well as the Advertising Law, the Management Standards for Disinfection Product Labels and Instructions, the Regulations on Supervision and Administration of Medical Devices, and other relevant laws and regulations.
All products sold are officially authorized. The actual formula (structure) of the products is consistent with the product packaging or instructions. Page titles are keywords used solely to match buyer search habits and do not represent the actual efficacy and characteristics of the products. The text, images, and video information on the page are solely for website optimization purposes. The actual ingredients and efficacy of the products are subject to the product packaging or instructions. Please be informed!


